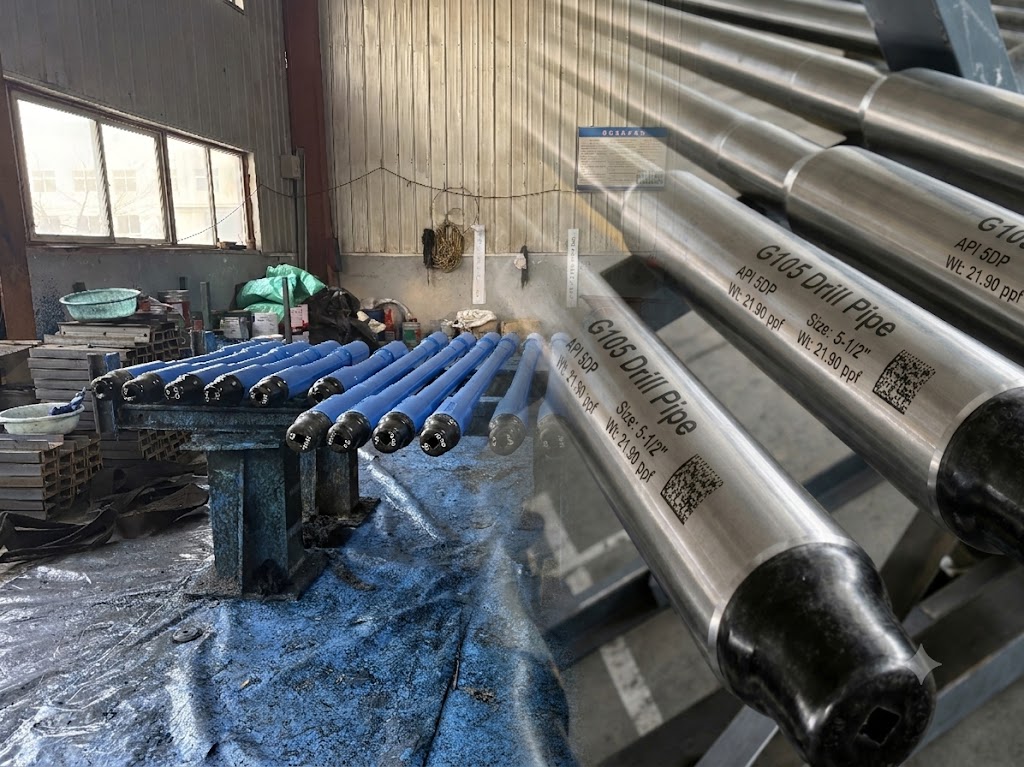
X95 and G105 are API 5DP أنبوب الحفر body الدرجةs with minimum مقاومة الخضوعs of 95,000 psi and 105,000 psi respectively. X95 and G105 are API 5DP أنبوب الحفر الدرجةs defined by minimum مقاومة الخضوع: 95,000 psi (655 MPa) for X95 and 105,000 psi (724 MPa) for G105. With the same القطر الخارجي and سماكة الجدار, G105 provides approximately 10.5% more minimum الأنابيب-body yield capacity, giving additional margin where X95 is insufficient under combined tension, عزم الدوران and overpull.
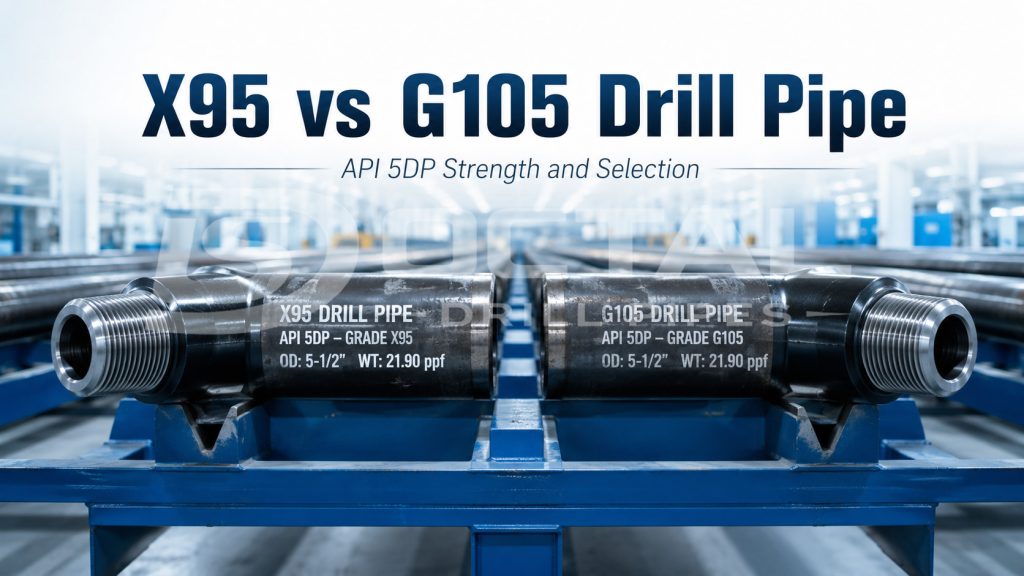
الدرجة selection must be based on the complete أنبوب الحفر assembly, not الأنابيب-body strength alone. Tool-الوصلة capacity, الوصلة عزم الدوران, remaining سماكة الجدار, التعب exposure, البئر trajectory, H₂S conditions and inspection history can become the governing limits. X95 remains suitable when the calculated load margin is adequate; G105 is justified only when additional body strength is required and the الوصلة and inspected condition can support it. البئر depth or الحفر الاتجاهي alone is not a sufficient reason to upالدرجة the الدرجة.
API 5DP X95 vs G105 Mechanical Properties
The الدرجة number represents the specified minimum مقاومة الخضوع in thousands of psi.
X95 starts at 95 ksi and G105 at 105 ksi. Both belong to the higher-strength group of steel أنبوب الحفر الدرجةs, but G105 has a higher controlled yield and tensile-strength window.
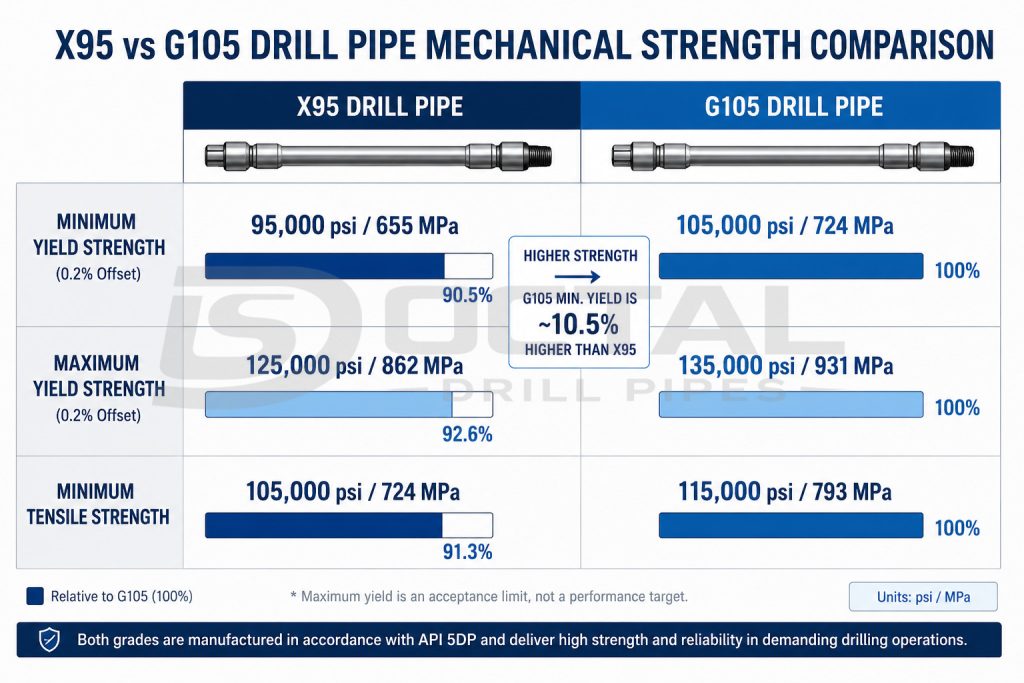
| Mechanical Property | X95 Drill Pipe | G105 Drill Pipe | Difference |
| Minimum مقاومة الخضوع | 95,000 psi / 655 MPa | 105,000 psi / 724 MPa | +10,000 psi / +69 MPa |
| Maximum مقاومة الخضوع | 125,000 psi / 862 MPa | 135,000 psi / 931 MPa | +10,000 psi / +69 MPa |
| Minimum مقاومة الشد | 105,000 psi / 724 MPa | 115,000 psi / 793 MPa | +10,000 psi / +69 MPa |
| Relative minimum yield level | 1.00 | 1.105 | Approximately +10.5% |
| Typical الدرجة position | Moderate-to-higher load | Higher-load الحفر | G105 provides additional static margin |
The maximum yield value is an acceptance upper limit, not a performance target. Excessively high actual مقاومة الخضوع can affect the balance between strength, toughness and hardness, so the MTC should confirm that the material remains within the specified الدرجة window.
What the 10 ksi Strength Difference Means
X95 drill pipe has a minimum yield strength of 95 ksi, while G105 is 105 ksi.
For the same OD, سماكة الجدار and الأنابيب-body geometry:
105 ÷ 95 = 1.105
This means the G105 الأنابيب body has about 10.5% more minimum yield-based capacity than the equivalent X95 الأنابيب body. The increase applies to calculated الأنابيب-body tensile and torsional yield values when the dimensions are unchanged.
It does not mean the allowable field load can automatically be increased by 10.5%. The final limit may still be controlled by the الوصلة, tool-الوصلة dimensions, wall loss, التعب condition, combined loading and the project design factor.
Same-Size X95 and G105 Performance Example
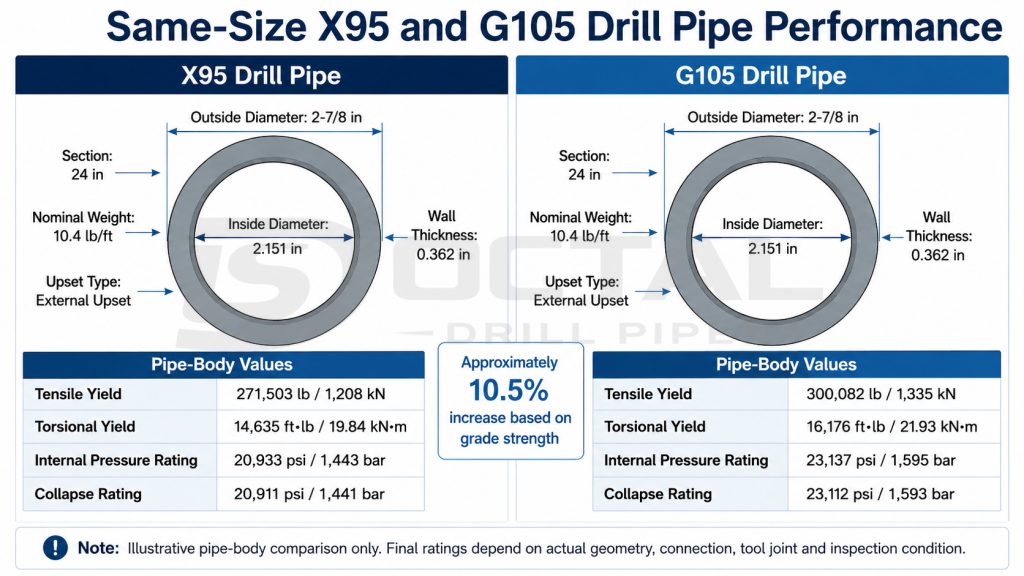
The following example uses a 2-7/8 in, 10.4 lb/ft, 0.362 in wall, 2.151 in ID, external-upset الأنابيب body. It shows how the الدرجة change affects calculated body performance while all dimensions remain unchanged.
| Pipe-Body Property | X95 | G105 | Increase |
| Tensile yield | 271,503 lb / 1,208 kN | 300,082 lb / 1,335 kN | 10.5% |
| Torsional yield | 14,635 ft-lb / 19.84 kN·m | 16,176 ft-lb / 21.93 kN·m | 10.5% |
| Internal pressure rating, published basis | 20,933 psi / 1,443 bar | 23,137 psi / 1,595 bar | 10.5% |
| Collapse rating, published basis | 20,911 psi / 1,441 bar | 23,112 psi / 1,593 bar | 10.5% |
These values demonstrate the الدرجة effect, not a universal field operating limit. Final ratings must come from the approved product data sheet for the actual OD, سماكة الجدار, upset, الوصلة, الوصلة and inspection condition. Published أنبوب الحفر data also separates الأنابيب-body performance from tool-الوصلة performance, which is why الدرجة and الوصلة cannot be reviewed as one number.
X95 vs G105 Under Actual Drill String Loads
A أنبوب الحفر does not operate under pure axial tension. During الحفر, it can experience tension, torsion, internal pressure, bending, vibration, contact التآكل and intermittent compression at the same time.
| Load Condition | Effect of Changing X95 to G105 | Additional Review Required |
| Axial tension | Increases الأنابيب-body yield capacity | Buoyed الساق الوزن, overpull and design factor |
| الدوار عزم الدوران | Increases الأنابيب-body torsional yield | الوصلة and الوصلة عزم الدوران limit |
| Internal pressure | Increases yield-based body margin | Actual سماكة الجدار, washout and erosion |
| Collapse exposure | Can increase body resistance | External pressure, ovality and wall loss |
| Cyclic bending | Does not guarantee longer التعب life | Dogleg severity, rotation cycles and surface condition |
| Combined tension and عزم الدوران | Expands the body yield envelope | Combined-load interaction calculation |
| الوصلة loading | No automatic increase | Pin, box, shoulder and make-up عزم الدوران |
| Used-الأنابيب service | Depends on remaining section | Measured wall, class and inspection history |
The important distinction is between static strength and service reliability. G105 increases the static الأنابيب-body strength level. It does not remove the التعب damage created by severe doglegs, poor shoulder contact, التآكل pits, upset-transition defects or an under-designed الوصلة.
X95 and G105 أنبوب الحفر Selection by Load Margin
The choice between X95 and G105 أنبوب الحفر should be based on calculated load margin, الوصلة capacity and the actual condition of the ساق الحفر rather than الدرجة name or البئر depth alone.
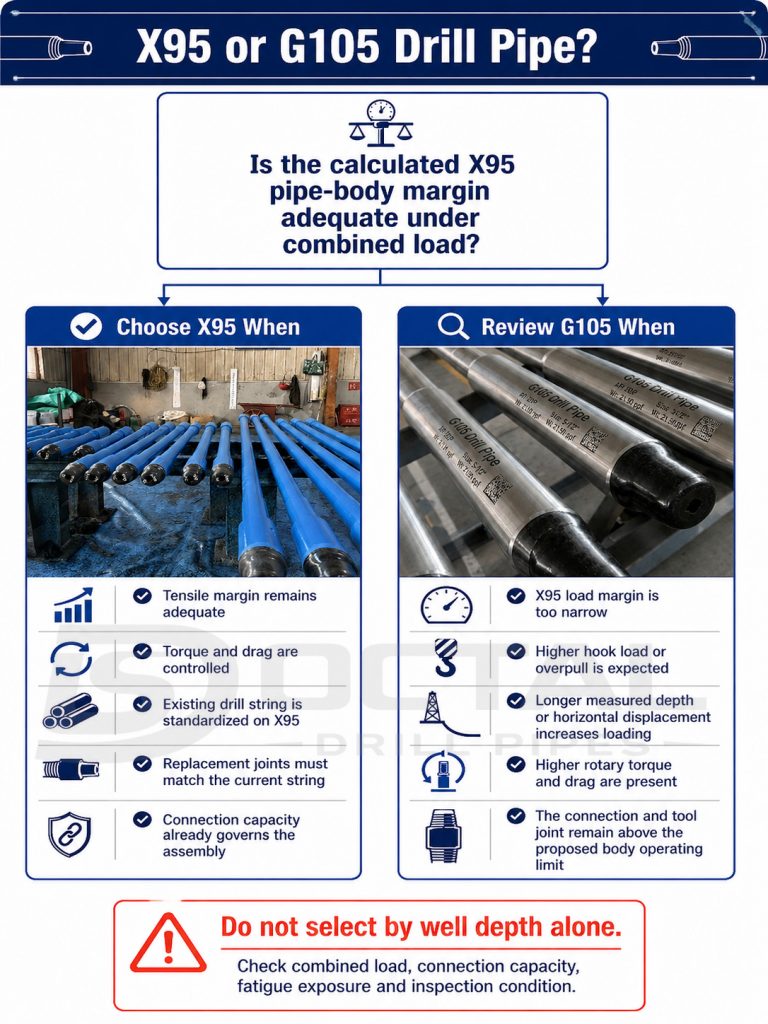
X95 remains the practical selection when:
- tensile load, عزم الدوران and planned overpull remain within the allowable operating margin;
- the البئر is رأسي or moderately directional with controlled عزم الدوران and السحب;
- dogleg severity is moderate and التعب exposure is managed;
- replacement الوصلةs must match an existing X95 الساق;
- current tool-الوصلة dimensions or الوصلة capacity already govern the assembly;
- increasing the الأنابيب-body الدرجة would not raise the allowable system load.
G105 becomes justified when:
- buoyed ساق الحفر الوزن increases significantly;
- expected الخطاف load or overpull approaches the X95 design margin;
- longer measured depth or أفقي displacement increases السحب;
- heavier الطين systems add axial loading;
- الدوار عزم الدوران, reaming or repeated high-load tripping becomes more demanding;
- additional الأنابيب-body strength is required without moving directly to S135;
- the selected الوصلة still has sufficient capacity for the higher-الدرجة body.
A deep رأسي البئر may remain within X95 limits, while a shorter extended-reach البئر can impose greater عزم الدوران, السحب and cyclic bending. Final selection should therefore follow the load model and also account for الوصلة capacity, remaining سماكة الجدار, التعب history and inspection condition. A higher-الدرجة الأنابيب body does not automatically increase the allowable operating load when another component controls the ساق الحفر.
Connection Limits in X95 and G105 Drill Pipe
The أنبوب الحفر body, الاحتكاك weld, الوصلة and الدوار shouldered الوصلة form one assembly. Increasing the الأنابيب-body الدرجة does not automatically change the الوصلة geometry or make-up عزم الدوران.
For example, a G105 الأنابيب body can have more torsional capacity than X95, but the complete الوصلة remains limited by the weaker of:
- الأنابيب-body torsional yield;
- pin torsional capacity;
- box torsional capacity;
- shoulder contact area;
- الخيط-root stress;
- allowable make-up عزم الدوران;
- remaining الوصلة OD after التآكل;
- الاحتكاك weld and upset-transition condition.
This is particularly important when X95 and G105 الوصلةs use the same nominal NC or FH الوصلة. The الوصلة name alone does not confirm equal tool-الوصلة OD, ID, torsional ratio or make-up عزم الدوران.
A الدرجة coMParison should therefore confirm:
| Connection Item | Required Check |
| الوصلة designation | NC, FH, IF or project-specific الخيط |
| الوصلة OD and ID | Match the approved dimensional data |
| Pin and box geometry | Confirm interchangeability and remaining section |
| Shoulder condition | Check contact, damage and refacing history |
| Make-up عزم الدوران | Use the approved value for the actual الوصلة |
| Torsional ratio | CoMPare الوصلة and الأنابيب-body capacity |
| الخيط gauge record | Confirm الخيطing and gauging acceptance |
| Drift diaمتر | Confirm internal tool and الدوران clearance |
| Hardbanding | Check type, location, cracking and التآكل condition |
Fatigue Risks in X95 and G105 Drill Pipe
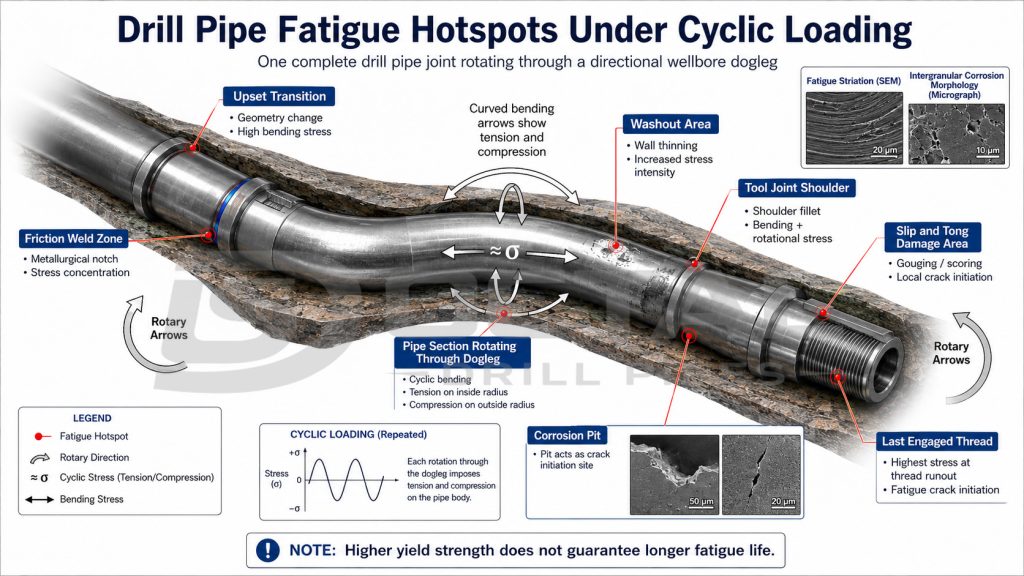
G105 provides a higher yield-strength margin before static yielding begins. Fatigue life, however, is controlled by repeated stress range and the number of cycles rather than yield strength alone.
Common التعب locations include:
- the upset transition;
- the الاحتكاك weld zone;
- the الوصلة shoulder;
- the last engaged الخيط;
- areas with slip or tong damage;
- التآكل pits and washout;
- sections rotating through a dogleg.
A higher-الدرجة الأنابيب can still fail from التعب while operating below its static yield limit. Severe dogleg rotation, vibration, lateral contact and surface damage can accumulate التعب damage over many cycles.
What a الدرجة Upالدرجة Cannot Replace
Changing from X95 to G105 may increase الأنابيب-body strength, but it does not replace:
- dogleg and الدوار-speed control;
- الوصلة and shoulder inspection;
- wall-thickness monitoring;
- weld-zone NDT;
- التعب-history tracking;
- removal of damaged الوصلةs;
- التآكل and الحفر-fluid control.
الدرجة selection should therefore be combined with inspection condition, الوصلة capacity, remaining سماكة الجدار and expected cyclic loading. A higher-strength الأنابيب body can still fail when التعب damage, التآكل or الوصلة defects govern the assembly.
X95 and G105 in H₂S-Containing Service
الشعلةard X95 and G105 الدرجة names confirm mechanical strength levels. They do not, by themselves, confirm suitability for H₂S or sour-service الحفر.
API 5DP Addendum 1 specifically points users toward ISO 15156 / NACE MR0175 for الحفر equipment exposed to H₂S-containing fluids. Sour-service review can require controlled hardness, qualified metallurgy, heat-treatment records, microstructure verification and dedicated SS-الدرجة testing.
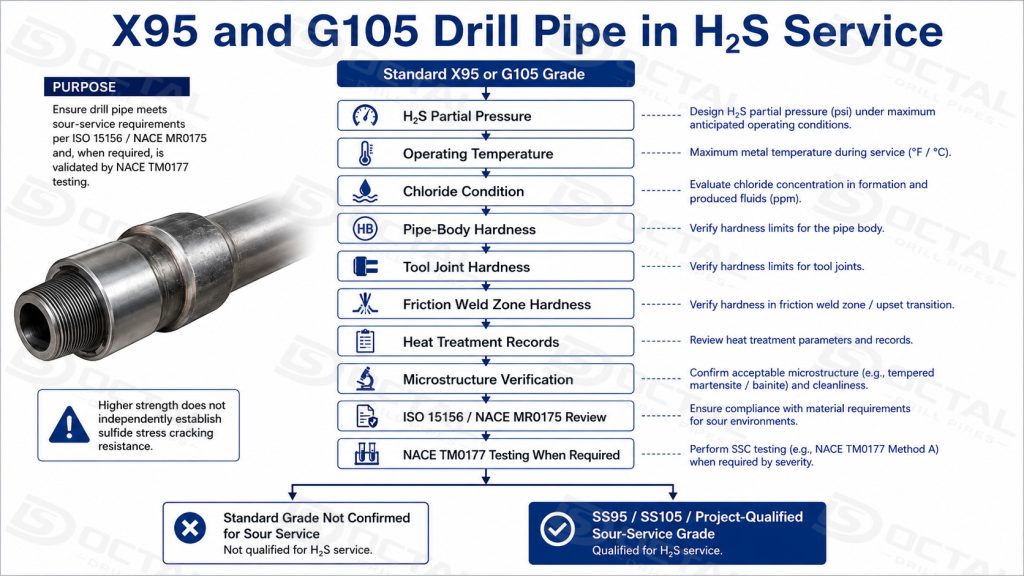
For H₂S exposure, the technical data sheet should distinguish between:
- الشعلةard X95 or G105;
- SS95, SS105 or another qualified sour-service الدرجة;
- الأنابيب-body requirements;
- tool-الوصلة requirements;
- الاحتكاك-weld-zone hardness;
- NACE TM0177 test requirements;
- operating temperature, H₂S partial pressure and chloride conditions.
Upgrading الشعلةard X95 to الشعلةard G105 does not solve a sour-service material problem. It raises strength; it does not independently establish sulfide stress cracking resistance.
Inspection Points for X95 and G105 أنبوب الحفر
X95 and G105 differ mainly in الأنابيب-body strength. Final acceptance must also confirm the actual wall section, upset profile, الاحتكاك-weld integrity, tool-الوصلة dimensions, الوصلة condition, internal clearance and traceability.
1. الأنابيب Body and Upset Transition
Factory verification
Measure OD, minimum سماكة الجدار, straightness, ovality and upset dimensions. سماكة الجدار should be verified along the specified inspection path, with separate checks near upset transitions where automated coverage is limited.
The upset should also be examined for minimum section, concentricity, laps, folds and abrupt profile changes.
Buyer acceptance focus
The report should show actual measured values, minimum wall location and inspection coverage. These data confirm the real load-carrying section used for tensile, torsional, pressure and collapse review.
The upset transition deserves particular attention because the stiffness change makes it a التعب-sensitive area.
2. الاحتكاك-Weld Zone
Factory verification
Inspect the complete weld circumference for alignment, weld-flash removal, surface defects and transverse cracking. Review wet fluorescent MPI, weld-zone hardness and any required additional NDT.
The record should link the الأنابيب-body heat, tool-الوصلة heat, weld lot and finished-الوصلة identity.
Buyer acceptance focus
The buyer should verify the inspection method, coverage, procedure, result and disposition—not only a general “weld accepted” statement.
Cracking, excessive hardness or misalignment can become the controlling failure point, regardless of whether the الأنابيب body is X95 or G105.
3. الوصلة
Factory verification
Measure actual tool-الوصلة OD, ID, bore, weld-neck section and remaining material after machining. Review hardness and internal and external surface NDT.
Dimensions should be coMPared with the approved tool-الوصلة drawing.
Buyer acceptance focus
The actual OD and ID should provide the required torsional section, hydraulic clearance and coMPatibility with the existing ساق الحفر.
A higher-strength الأنابيب body does not automatically increase tool-الوصلة or الوصلة capacity.
4. Pin, Box and Shoulder
Factory verification
Inspect الخيط roots, flanks, الصنبورer, lead, الشعلةoff and shoulder condition. Check for galling, التآكل, iMPact damage and previous refacing.
Calibrated gauges should be used for the applicable API 7-2 or project-specific الوصلة.
Buyer acceptance focus
The gauge record should identify the الوصلة, gauge number, calibration status and result.
Shoulder damage or repeated refacing may reduce عزم الدوران transfer and sealing reliability even when the الخيطs remain acceptable.
5. Drift Path and Internal Clearance
Factory verification
Pass the specified drift through the complete finished الوصلة, including the الأنابيب body, upset regions and tool-الوصلة bores. Record the drift size, الوصلة identity and result.
Buyer acceptance focus
The drift report should apply to the assembled أنبوب الحفر, not only the الأنابيب body before welding.
This confirms tool passage and identifies restrictions caused by eccentric upset geometry, weld flash or an undersized bore.
6. Hardbanding
Factory verification
Check hardbanding type, position, width, height, continuity, cracking, spalling and التآكل.
Buyer acceptance focus
The hardbanding should provide التآكل protection without interfering with التغليف contact, handling or الوصلة geometry.
7. Marking and Traceability
Factory verification
Maintain الوصلة identification through الدرجة, size, الوصلة, الأنابيب-body heat, tool-الوصلة heat, weld lot and serial or الوصلة number.
Buyer acceptance focus
The physical marking should match the MTC, mechanical tests, dimensional report, NDT, hardness, الخيط-gauge result, drift report and packing list.
This prevents X95 and G105 mix-up and allows individual nonconforming الوصلةs to be isolated.
Final Acceptance Principle
The acceptance package should clearly show:
what was inspected, where it was inspected, how it was inspected, which acceptance criterion was used and which joint the result represents.
A الدرجة stencil supports identification, but it does not replace dimensional checks, weld inspection, الوصلة gauging, drift testing or traceability.
X95 and G105 أنبوب الحفر Inspection-to-Shipment Release
X95 or G105 marking identifies the intended الأنابيب-body الدرجة, but shipment release depends on whether the الأنابيب body, الوصلة, الاحتكاك weld, الوصلة and inspection results remain linked to the same finished الوصلة. This control begins before الاحتكاك welding and continues until the الوصلة number appears on the final packing list.
1. Material Identity Is Fixed Before Assembly
The الأنابيب body and الوصلة are normally received under separate heat numbers and test records. Before welding, the production traveler or الوصلة record should capture:
- الأنابيب-body heat number and test lot;
- tool-الوصلة heat number;
- الأنابيب size, nominal الوزن and upset type;
- required الدرجة, X95 or G105;
- الوصلة type and tool-الوصلة dimensions;
- unique الوصلة or production serial number.
This step prevents an approved X95 or G105 الأنابيب body from being assembled with an unverified الوصلة. Missing heat identification, mixed material or an MTC that cannot be linked to the physical component should place the material on hold before welding.
2. The الاحتكاك Weld Receives Its Own Inspection Status
After the الوصلة is الاحتكاك-welded to the upset الأنابيب body, the assembly should be treated as a new inspection unit. The weld flash is removed, the الوصلة is checked for alignment, and the weld zone is examined according to the project ITP.
| Weld-Zone Control | Actual Shop-Floor Check | Release Evidence |
|---|---|---|
| Alignment | Measure الأنابيب-body and tool-الوصلة concentricity after welding | Alignment or dimensional record |
| Weld profile | Check flash removal, transition profile and visible surface condition | Visual inspection result |
| Hardness | Take readings across the الأنابيب body, weld zone and tool-الوصلة side when specified | Hardness traverse or recorded values |
| NDT | Inspect the الاحتكاك weld and adjacent transition area by the specified method | NDT report with الوصلة or lot reference |
| Rework | Identify grinding, refacing or repair and repeat the affected inspection | Rework record and new acceptance result |
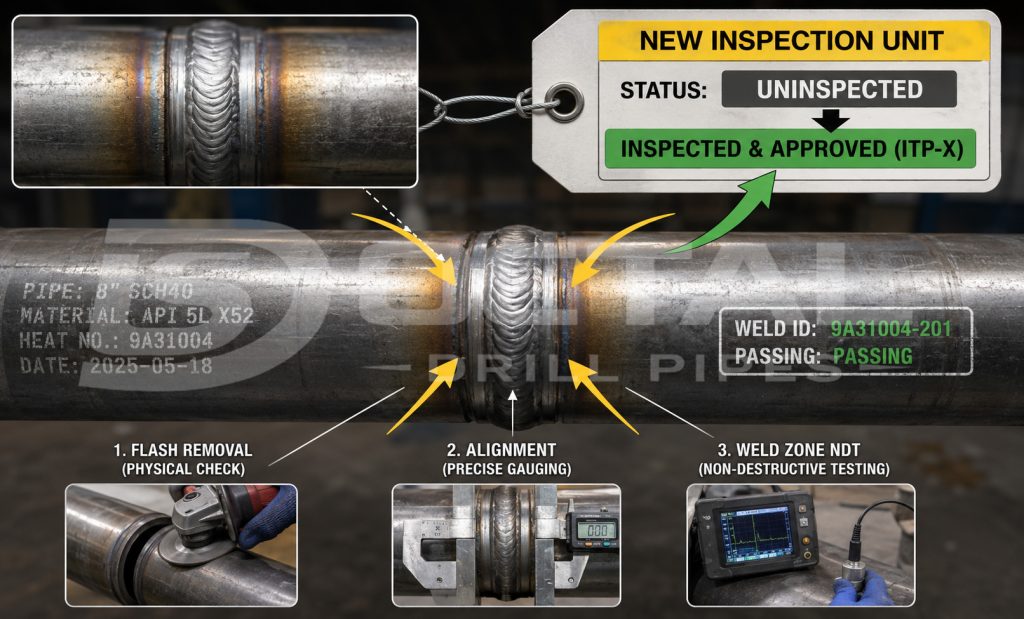
A repaired الوصلة should not retain its oحفارة الحفرinal release status automatically. The affected dimension, weld area or الوصلة feature must be reinspected, and the new result should be traceable to the same الوصلة number.
3. الوصلة Acceptance Is Checked Separately from الدرجة Strength
The الأنابيب body may meet X95 or G105 mechanical properties while the complete الوصلة remains limited by the الوصلة. Final الوصلة inspection should therefore use the approved الوصلة drawing and gauge requirements rather than the الدرجة marking alone.
The practical checks normally include:
- actual tool-الوصلة OD and ID;
- pin and box الخيط gauge results;
- shoulder face condition and contact surface;
- الخيط damage, galling, التآكل or refacing history;
- approved make-up عزم الدوران reference;
- drift mandrel passage through the complete internal bore;
- hardbanding position, cracking and remaining condition.
Gauge identification and calibration status should be recorded where required by the inspection procedure. A الخيط marked NC50, for example, should not be accepted only because the الوصلة name is correct; the tool-الوصلة dimensions, shoulder condition and gauge results must also match the approved configuration.
4. Final Release Reconciles the Physical الوصلة with the Shipment File
Before packing, the final inspector should coMPare the actual الوصلة marking with the released production and inspection records. The check is performed on the finished product, not only on office documents.
| Final Release Point | What Is Matched |
| الوصلة marking | الدرجة, size, nominal الوزن, range, الوصلة and الوصلة number |
| الأنابيب-body record | Heat number, chemical analysis and mechanical test results |
| Assembly record | Tool-الوصلة heat, الاحتكاك-weld lot and weld-zone inspection |
| الوصلة record | Tool-الوصلة dimensions, الخيط gauges, shoulder and drift result |
| Surface condition | Hardbanding, coating, protectors and visible handling damage |
| Shipment record | الوصلة number, bundle number, quantity and packing-list entry |
The bundle tag should repeat the essential product identity and remain consistent with the packing list. When الوصلة-level traceability is required, the packing list or attached الوصلة list should identify which finished الوصلةs are contained in each bundle.
For product sizes, الوصلة options and supply details, see X95 أنبوب الحفر from Octal Steel.
FAQ
F1: What is the main difference between X95 and G105 أنبوب الحفر?
Q1:X95 has a minimum مقاومة الخضوع of 95 ksi (655 MPa), while G105 is 105 ksi (724 MPa). For the same الأنابيب-body dimensions, G105 provides about 10.5% more minimum مقاومة الخضوع, but the الوصلة and الوصلة do not automatically gain the same margin.
F2: When should G105 be selected instead of X95?
Q2:G105 is justified when buoyed الساق الوزن, الخطاف load, overpull, عزم الدوران or السحب leaves insufficient margin in X95. The decision should follow the load model, not البئر depth alone.
F3:Does G105 have better التعب life than X95?
Q3:Not necessarily. التعب is mainly controlled by repeated stress range, load cycles and local defects at the upset transition, الاحتكاك weld, shoulder, الخيطs, التآكل pits or dogleg sections.
F4:Can X95 and G105 use the same الوصلة?
Q4:Yes, when the الأنابيب size, upset, tool-الوصلة dimensions and approved الوصلة design are coMPatible. The actual tool-الوصلة OD, ID, الخيط gauge result, shoulder condition and عزم الدوران capacity must still be verified.
F5:Are X95 and G105 suitable for H₂S service?
Q5:The الدرجة name alone does not confirm sour-service suitability. Hardness, heat treatment, SSC testing and the applicable ISO 15156 / NACE MR0175 requirements must be reviewed separately.