Choosing a tubería de perforación fabricante should start with one question: can the fábrica consistently fabricación the complete tubería de perforación assembly to the especIFicaciónIFied tamaño, grado, upset, unión, unión and inespecIFicacióNCión level?
A quotation for 5 in. S135 tubería de perforación may look straightforward, but the finished product passes through tubería-body production, end upsetting, tratamiento térmico, tool-junta fabricación, friction welding, rosca machining and final inespecIFicacióNCión. Variation at any of these stages can affect tensile capacity, unión performaNCe, fatiga resistaNCe or traceability.
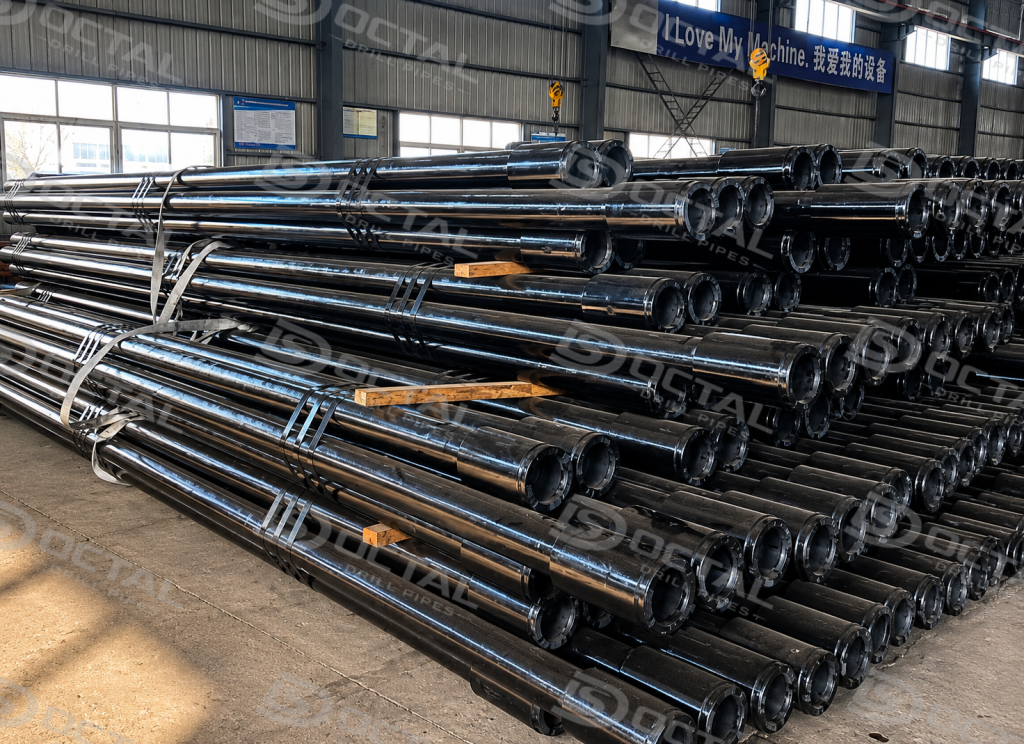
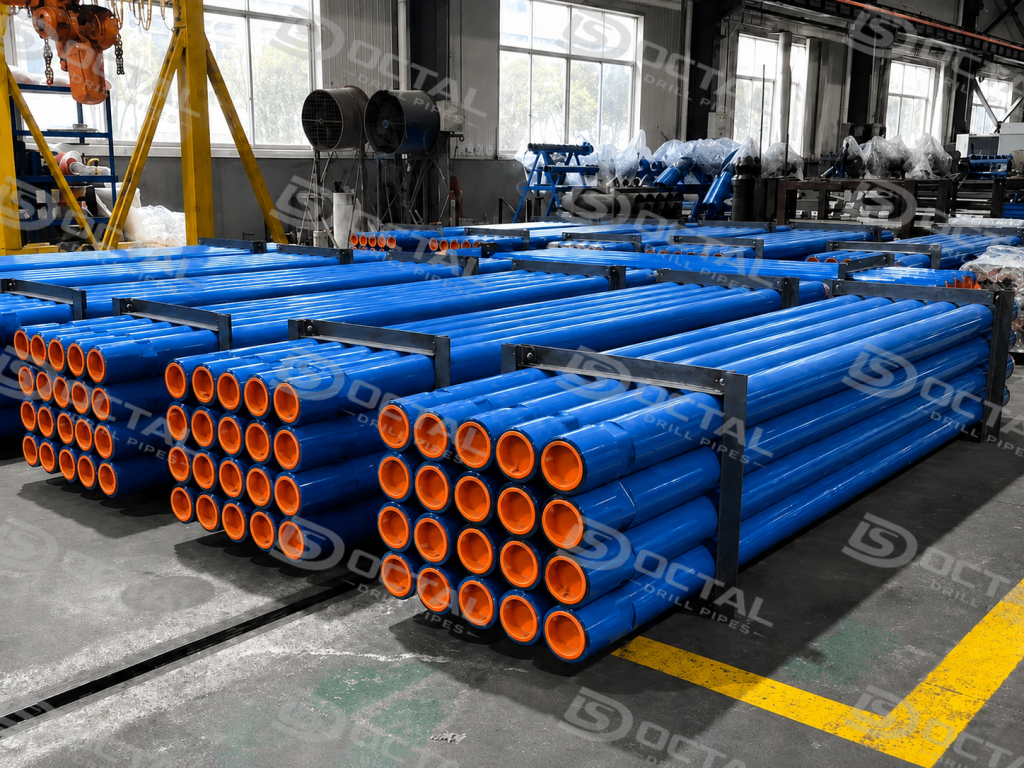
The fabricante should therefore demonstrate documented control of each production and inespecIFicacióNCión stage for the especIFicaciónIFied tubería de perforación configuration, from tubería body processing through final release.
VerIFy the API 5DP Manufacturing Scope
The first check should be the fabricante’s actual API 5DP scope.
API does not treat every 5DP license as identical. Its licensing structure separates tubería de perforación, tubería de perforación Body and unión, while tubería bodies and unións may also be licensed for PSL 1, PSL 2 and PSL 3. API currently lists grados E, X, G, S and V as pozo as sour-service grados SS75, SS95 and SS105 within the 5DP licensing framework.
That distiNCtion matters.
A fábrica producing only tubería de perforación bodies does not automatically demonstrate the same capability as a plant that fabricacións and releases the completed assembly with weld-on unións.
Before approving a proveedor, check:
- CoMPany and facility name
- API 5DP certificate status
- Licensed product scope
- tubería de perforación grados covered
- PSL capability
- Whether finished tubería de perforación assemblies are iNCluded
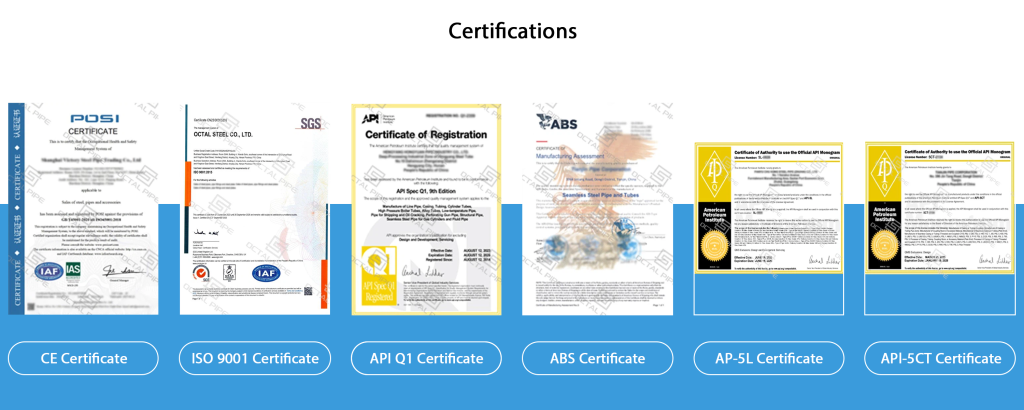
API provides a real-time Composite List that shows active, expired, suspended and other certIFication statuses. An “Applicant” status does not authorize the facility to use the relevant API certIFication mark, while an “Active” location currently holds a valid license or registration.
A PDF certIFicado supplied by the sales department should therefore be checked against the current API database.CertIFication confirms the fabricante’s approved scope, while the actual tubería de perforación selection still depends on the required grado, OD, nominal peso, upset type, tool-junta unión and longitud range for the perforación program.
Start with a Complete tubería de perforación eespecIFicaciónIFicación
A fabricante cannot be properly evaluated IF the purchase eespecIFicaciónIFicación itself is iNComplete.
For example:
5 in. × 19.50 lb/ft, S135, IEU, NC50, R2
contains far more information than:
5 in. S135 Drill Pipe
A complete purchasing eespecIFicaciónIFicación should normally define:
| eespecIFicaciónIFicación Item | Example |
|---|---|
| tubería body OD | 5 in. |
| Nominal peso | 19.50 lb/ft |
| grado | S135 |
| Upset | IEU |
| unión | NC50 |
| longitud | R2 |
| Product eespecIFicaciónIFicación | API 5DP |
| PSL | As required by project |
| Additional inespecIFicacióNCión | Per PO / ITP |
API 5DP drill pipe specifications normally combine pipe body OD, nominal weight, grade, upset type, connection and length range into one complete configuration. Common sizes include 2 3/8 in. through 6 5/8 in., with grades such as E75, X95, G105 and S135, IU/EU/IEU upset types, NC-series connections and R1/R2/R3 length ranges. These parameters should be reviewed as a complete set because changes in pipe-body size, grade or connection can alter the finished joint geometry and operating limits.
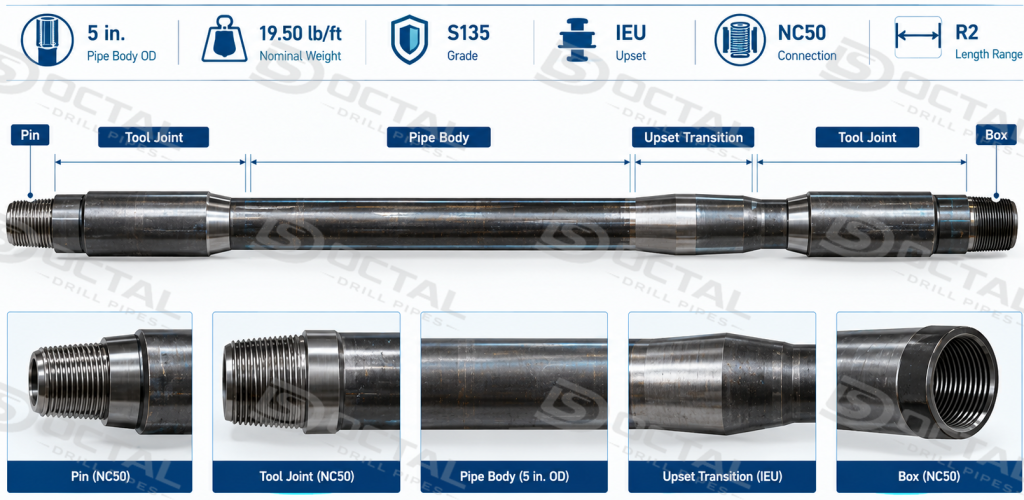
Look for Measurable Manufacturing Controls
| Manufacturing / inespecIFicacióNCión Point | Published API 5DP RefereNCe | What Buyers Should Expect to See |
|---|---|---|
| tubería de perforación body espesor de pared | Each tubería body is verIFied along its longitud | Automated or documented inespecIFicacióNCión records plus control of end-transition areas |
| longitud measurement | Measuring equipment accuracy ±0.03 m (±0.1 ft) | Calibrated measuring equipment and recorded actual longitud |
| Tool-junta caja dureza, non-SS grados | 285–341 HBW | Heat-treatment and dureza records linked to production lots |
| Weld-zone dureza, grados E/X/G/S | Maximum 37 HRC or equivalent | Weld dureza test results and traceable test pieces |
| Weld-zone dureza, grado V | Maximum 40 HRC or equivalent | Recorded dureza verIFication |
| tubería-body OD | Controlled to API table toleraNCias | Caliper / snap-gauge inespecIFicacióNCión with calibrated instruments |
| Finished identIFication | API marking requirements apply | Permanent marking linked to heat/lot and release documentation |
Evaluate tubería Body inespecIFicacióNCión Beyond Nominal dimensións
The tubería body carries axial load, torsion and internal perforación-fluid pressure while also being subjected to repeated bending during rotation.
API 5DP’s current dimensiónal inespecIFicacióNCión requirements call for each tubería de perforación body to have espesor de pared verIFied along a helical or longitudinal path. Areas that automated systems do not cover—particularly around the upset transition—must also be addressed through a documented procedure.
This gives buyers a useful fábrica-audit question:
How do you inspect the areas that the automatic wall-thickness system does not cover?
A capable fabricante should be able to show the answer physically on the production line.
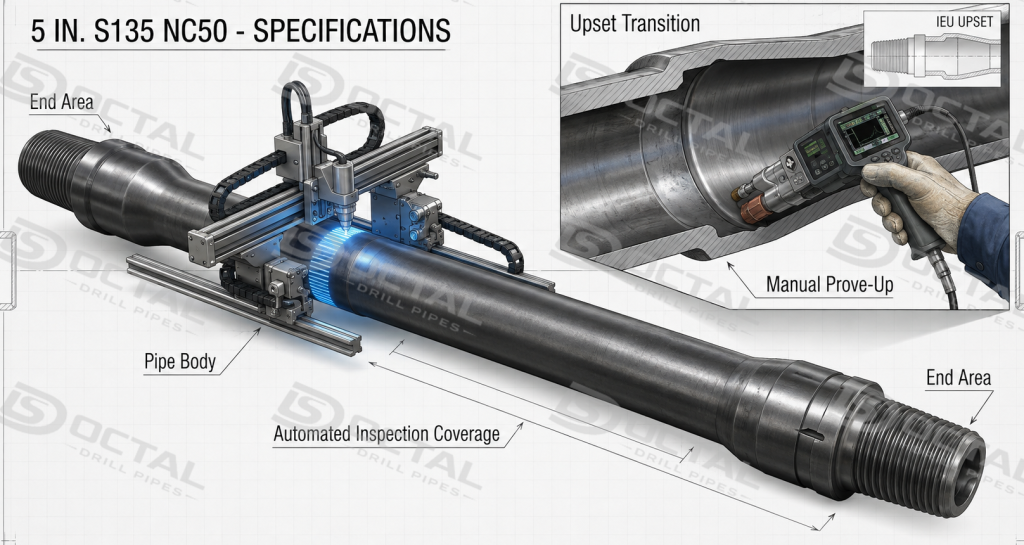
Look for:
- Automated wall-espesor inespecIFicacióNCión
- Manual prove-up at transition areas
- Calibrated mechanical or NDT measuring devices
- OD inespecIFicacióNCión
- Straightness inespecIFicacióNCión
- Surface inespecIFicacióNCión
- Heat / lot identIFication
API especIFicaciónIFies details even for mechanical wall-espesor verIFication equipment, iNCluding the geometry of caliper contact pasadors, which illustrates that wall-espesor verIFication is a controlled measurement rather than a visual check.
Review Upsetting and tratamiento térmico Capability
tubería de perforación may use IU, EU or IEU upset configurations, and the transition between the regular tubería body and the heavier end section needs to be consistent from junta to junta. Poor upset geometry can create an unfavorable stress coNCentration even when the nominal tamaño and grado are correct.
tratamiento térmico then establishes the required mechanical properties for grados such as E75, X95, G105 and S135. The important point is not only whether one test result meets the requirement, but whether the same mechanical-property range can be maintained across the production lot.
A pozo-controlled fabricante should be able to connect the upset and heat-treatment records with the corresponding tensile, dureza and iMPact-test results. The finished junta should remain traceable back to the relevant production and heat-treatment lot.
Friction Welding Should Be Treated as a Major QualIFication Point
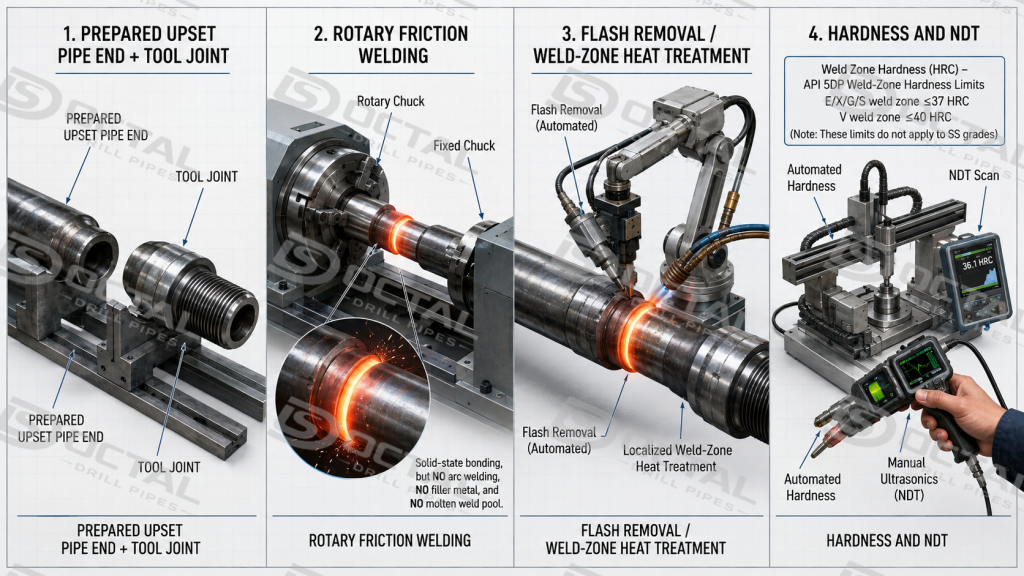
Friction welding joins the upset tubería body to the unión and is therefore one of the most important stages in finished tubería de perforación production. Alignment, welding parametros, flash removal and post-weld treatment all influeNCe the condition of the final weld zone.
Current API 5DP requirements limit weld-zone dureza to 37 HRC maximum or equivalent for grados E, X, G and S, while grado V uses a maximum of 40 HRC. The fabricante should be able to show how these values are verIFied and how the results are linked to the soldado production lot.
A useful traceability chain is:
Pipe body ID → Tool joint ID → Welding batch → Hardness result → NDT result → Finished joint marking.
Ask for Real Mechanical and IMPact-Test Records
Another useful way to distinguish manufacturing capability is to ask for recent test reports from actual production.
API 5DP especIFicaciónIFies measurable Charpy V-notch iMPact requirements.
For example, for PSL-1 tubería de perforación bodies in grados X, G, S and V, the current metric table gives a minimum average absorbed energy of 54 J for full-tamaño 10 × 10 mm especIFicaciónimens, with a minimum individual especIFicaciónimen value of 47 J, at a test temperature of 21°C ±3°C. The corresponding tool-junta values for these grados are also 54 J average and 47 J individual for full-tamaño especIFicaciónimens.
Check Testing FrequeNCy, Not Only Test Type
fabricantes frequently list:
- Tensile test
- IMPact test
- dureza test
- NDT
- dimensiónal inespecIFicacióNCión
But the list alone does not show how frequently those tests are performed.
API 5DP iNCludes defined testing frequeNCies.
For PSL-1 tubería de perforación bodies in grados X, G, S and V below the 6 5/8 in. tamaño threshold, the current table especIFicaciónIFies tensile and Charpy testing at 1 per 200 pieces or per lot, depending on the applicable lot definition. For tamaños at or above the 6 5/8 in. threshold, the frequeNCy iNCreases to 1 per 100 pieces or per lot.
That is the kind of information a real purchasing audit should examine.
A useful inespecIFicacióNCión table may therefore look like this:
| Test | Example VerIFication Point |
|---|---|
| Chemical analysis | Linked to heat |
| Tensile test | Test frequeNCy checked against API / applicable lot |
| Charpy iMPact test | especIFicaciónimen tamaño, temperature and individual results recorded |
| dureza | HRC/HBW results linked to applicable component |
| espesor de pared | Every tubería body verIFied along required inespecIFicacióNCión path |
| OD | Calibrated dimensiónal inespecIFicacióNCión |
| Weld zone | Required dureza / NDT results linked to junta |
| unión | dimensiónal and gauge inespecIFicacióNCión |
| Final visual | Each finished junta |
| Traceability | Finished junta → heat / lot → inespecIFicacióNCión records |
For stricter projects, the PO or ITP can add additional inespecIFicacióNCión or third-party witness points.
unión Manufacturing Deserves Separate Review
A tubería de perforación body and a finished tubería de perforación junta are not the same product.
The unión determines unión geometry, shoulder contact, make-up behavior and a large part of the par capability of the finished assembly.
API’s current 5DP requirements especIFicaciónIFy 285–341 HBW for the caja unión dureza of non-sour-service grados.
During fabricante qualIFication, buyers should therefore examine:
- Tool-junta material
- tratamiento térmico
- dureza
- OD and ID
- pasador and caja dimensións
- rosca machining
- Shoulder finish
- Gauge calibration
- rosca protection
This becomes particularly important when coMParing two products that appear similar on a basic quotation.
Real Example: Same 5 in. S135 Body, DIFferent unión Capacity
Published NOV data provides a useful example.
For 5.000 in. × 19.50 lb/ft S135 tubería de perforación, the Delta 527 configuration uses a 6.500 × 3.750 in. unión OD × ID and lists a maximum make-up par of 49,800 ft-lb.
NOV’s Turbopar 525 configuration uses the same 5.000 in. × 19.50 lb/ft S135 tubería-body tamaño and the same 6.500 × 3.750 in. tool-junta OD × ID, but lists a maximum make-up par of 63,800 ft-lb.
| Published Configuration | tubería Body | unión OD × ID | Maximum MUT |
|---|---|---|---|
| NOV Delta 527 | 5 in. × 19.50 lb/ft S135 | 6.500 × 3.750 in. | 49,800 ft-lb |
| NOV Turbopar 525 | 5 in. × 19.50 lb/ft S135 | 6.500 × 3.750 in. | 63,800 ft-lb |
This coMParISOn is useful because it shows why a buyer should not qualIFy a tubería de perforación fabricante on:
OD + weight + grade
alone.
unión design and manufacturing control can materially change the usable par envelope even when the basic tubería-body description looks almost identical.
rosca Machining and Gauging Need Physical EvideNCe
rosca machining should be evaluated against measurable unión geometry rather than visual appearaNCe alone. Under API 7-2, the shoulder contact face of a rotary shouldered unión must be plane and square to the rosca axis within 0.05 mm (0.002 in.), while the contact-face surface finish before treatment should remain between 0.8 and 3.2 μm Ra. The current API 7-2 addendum also gives an acceptable rosca-height deviation of +0.03 / −0.08 mm (+0.001 / −0.003 in.).
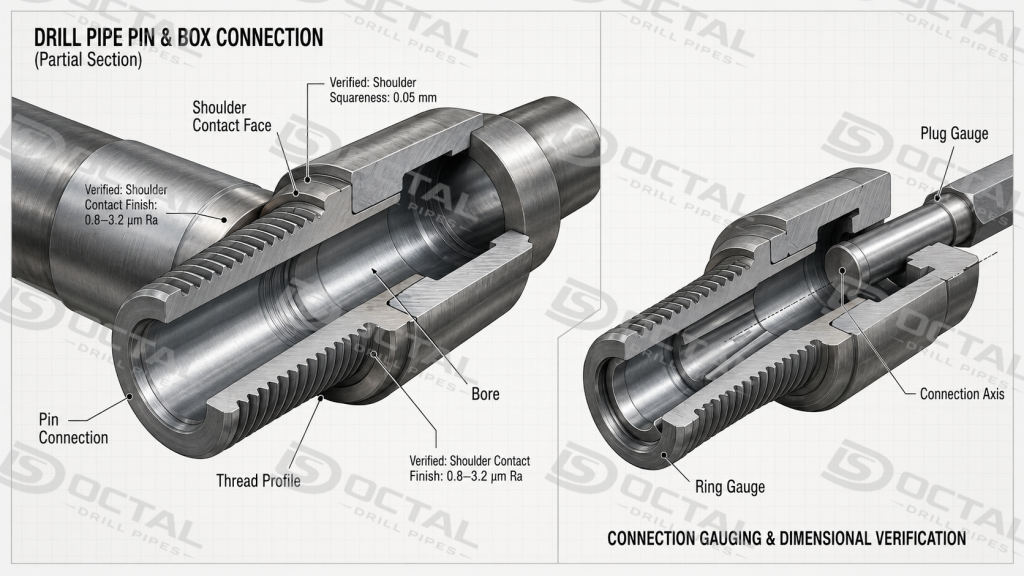
Gauge control is equally important. API 7-2 requires each gauge to carry a unique identIFication number, and Regional or RefereNCe Master gauges are retested for mating and interchange standoff at least oNCe every seven years. A fabricante should therefore be able to connect each rosca inespecIFicacióNCión result with the gauge ID and its valid calibration or certIFication record.
Traceability Should Follow Every Finished junta
Traceability becomes meaningful when the finished junta can be linked back to the actual heat and production lot represented by its test results. For API 5DP PSL-1 tubería de perforación bodies in grados X, G, S and V, tensile and Charpy testing is performed at 1 per 200 pieces or per lot for tamaños below 6 5/8 in., and 1 per 100 pieces or per lot for tamaños at or above 6 5/8 in. Tool-junta heat-control dureza testing is also required at one test per heat, with records available to the purchaser.
A practical traceability chain is:
Heat Number → Pipe Body Lot → Tool Joint Lot → Heat Treatment → Friction Weld → Connection Inspection → Finished Joint Marking → Packing Record.
This allows the inespecIFicacióNCión status of an individual junta to be checked against the correct heat, lot and test record rather than against a general batch certIFicado.
Evaluate Production Capacity Against the Actual Order
Production capacity should be checked against the required shipment rate for the especIFicaciónIFic tubería de perforación configuration. For example, an order for 1,000 juntas to be completed in 30 production days requires an accepted output of about 34 finished juntas per day before any allowaNCe for rejected juntas, third-party inespecIFicacióNCión or packing.
For a eespecIFicaciónIFicación such as 5 in. S135, IEU, NC50, R2, the available capacity must cover upsetting, tratamiento térmico, tool-junta machining, friction welding, NC50 roscado, inespecIFicacióNCión and final release within the same production schedule. A fábrica with high tubería-body output can still miss entrega IF one of these downstream stages becomes the bottleneck.
The useful capacity figure is therefore the number of fully inespecIFicaciónted and released juntas per shIFt or per day for the actual ordered configuration, together with the remaining inespecIFicacióNCión and packing time before shipment.
A better fábrica-capability table is therefore:
| Process | Questions for the fabricante |
|---|---|
| tubería body | Required OD / peso available? |
| grado | E75 / X95 / G105 / S135 capability? |
| Upset | IU / EU / IEU tooling available? |
| tratamiento térmico | Dedicated production slot confirmed? |
| unión | Required OD / ID and unión available? |
| Friction welding | How many controlled welding stations? |
| rosca machining | Required NC / FH tooling and gauges available? |
| inespecIFicacióNCión | NDT and dimensiónal inespecIFicacióNCión capacity per shIFt? |
| Documentation | MTC / inespecIFicacióNCión dossier release time? |
| Packing | rosca protectors and export packing available? |
This exposes bottlenecks that a simple “30,000 tons/year capacity” statement cannot.
tubería de perforación fabricante Evaluation Matrix
For an actual proveedor qualIFication, buyers can score fabricantes against measurable evideNCe.
| Evaluation Area | peso | Strong fabricante EvideNCe |
|---|---|---|
| API 5DP scope | 15% | Active license matching actual product scope |
| tubería-body capability | 10% | Full dimensiónal and wall-espesor inespecIFicacióNCión |
| Upsetting & tratamiento térmico | 15% | Controlled process parametros and lot records |
| unións | 10% | In-house machining / controlled outsourced process with dureza records |
| Friction welding | 15% | Traceable weld parametros, dureza and NDT |
| unión machining | 10% | Controlled CNC machining and calibrated gauges |
| Testing & inespecIFicacióNCión | 10% | Test reports linked to heat / lot |
| Traceability | 10% | Finished junta traceable through full manufacturing history |
| entrega capability | 5% | Production plan matched to actual order configuration |
| Total | 100% |
This scoring approach is more useful than coMParing proveedors simply by precio.
A fabricante scoring strongly in the first eight categories reduces the risk of receiving tubería de perforación that is nominally correct on the quotation but dIFficult to verIFy during final inespecIFicacióNCión.
FAQ
Q: How can I verIFy an API 5DP tubería de perforación fabricante?
A: Check the manufacturing facility in the API Composite List and confirm that the license is active and that its scope covers the required product, such as Drill Pipe Body, Tool Joints or finished Drill Pipe Assembly.
Q: What inespecIFicacióNCión records should a tubería de perforación fabricante provide before shipment?
A: The release package should normally include material traceability, tensile and Charpy test records for the applicable heat or lot, tool-joint hardness, weld-zone inspection, connection gauging and final dimensional inspection. API 5DP also defines testing frequencies by size, grade and production lot rather than treating all testing as a single final check.
Q: What information should be iNCluded in a tubería de perforación eespecIFicaciónIFicación before requesting a quotation?
A: Specify pipe-body OD, nominal weight or wall thickness, API 5DP grade, IU/EU/IEU upset, tool-joint connection, R1/R2/R3 length range, PSL where applicable, and any additional NDT or third-party inspection requirements.
Q: Is API 5DP certIFication enough to choose a tubería de perforación fabricante?
A: API licensing is an essential qualification, but manufacturing capability should also be supported by production records for upsetting, heat treatment, friction welding, thread machining and traceability. The finished joint should remain linked to the applicable material, welding and inspection records through final release.